IHI TRX160 Compressor — Major Overhaul at an ASU Plant
Major overhaul of an IHI TRX160 three-stage centrifugal air compressor for an ASU (air separation) plant: bull gear & bearings replacement, new intercoolers and oil cooler, diffuser replacement, cleaning and re-coating of the gas path — with full inspection record, surge test and coupling alignment data. Carried out by Turbomax engineers.
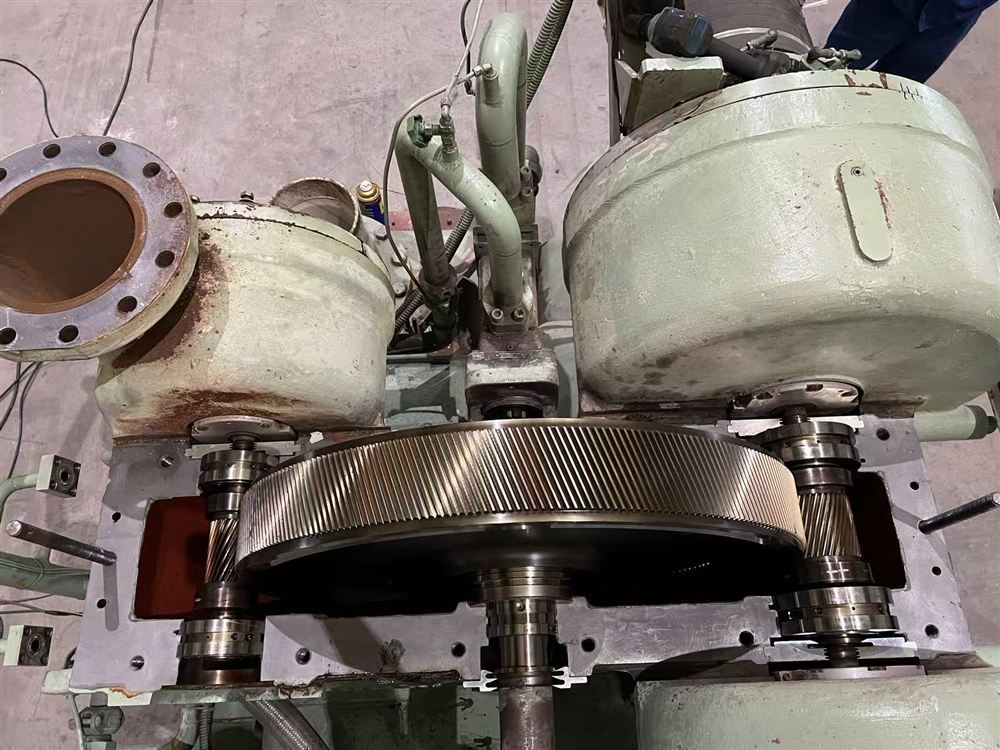
Machine background
This IHI TRX160 oil-free centrifugal air compressor supplies instrument and process air to an ASU (air separation) plant. When its performance kept falling and the discharge pressure could no longer hold at full load, the major overhaul was carried out at the customer's site — by then with roughly 34,700 running hours (about 31,000 loaded hours, 517 starts) on the counter.
| Model | IHI TRX160 (three-stage centrifugal air compressor) |
| Discharge pressure | 0.8 MPa class |
| Compression stages / gas | 3 stages / air |
| Motor | 6,600 V, approx. 186 A loaded |
| Running time at overhaul | approx. 34,700 hours |
Condition found during overhaul
- Bull gear & pinion gears — tooth flank abrasion on the bull gear and both pinion gears; the worn bull gear was replaced with a new one
- Bearings — bull gear bearing already unusable, high-speed and low-speed pinion bearings worn — all replaced with new
- 3rd-stage diffuser — heavy gas corrosion and cavitation, replaced with a new one; the 2nd-stage diffuser also shows early cavitation (recommended for next overhaul)
- Coolers — 1st-stage cooler housing leaking water and both intercoolers heavily fouled; two new air coolers and a new oil cooler installed
- Impellers & scrolls (1st/2nd/3rd stage) — lots of hard dust deposits, scroll casings seriously corroded — cleaned and re-coated
- Piping — hard dust inside the 2nd/3rd-stage inlet pipes; suction piping seriously rusted — cleaned and re-coated
- Seals — all 1st/2nd/3rd-stage air seals and oil seals replaced with new
- Consumables — intake air filter elements heavily dust-loaded (replaced), oil tank dirty (cleaned), oil filter replaced after oil-line flushing
Photos from the job
The complete photo record from the overhaul report — every stage's scroll, scroll house, impeller, coolers, gearbox, diffusers, piping and accessories, shown as found / after cleaning / after re-coating (or dye penetrant check):
1. 1st stage scroll — cleaning & re-coating
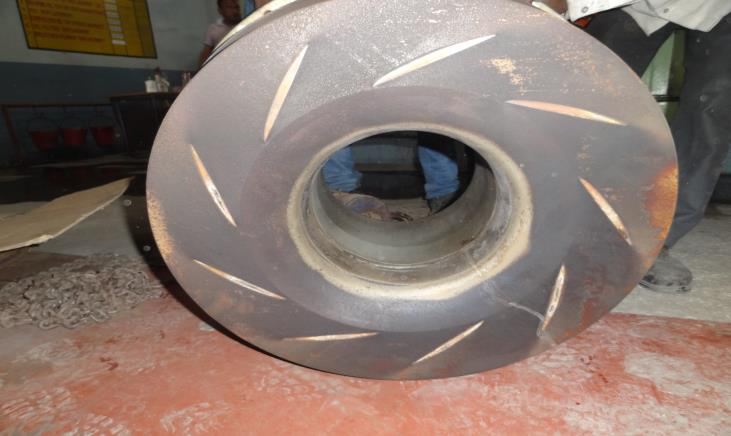
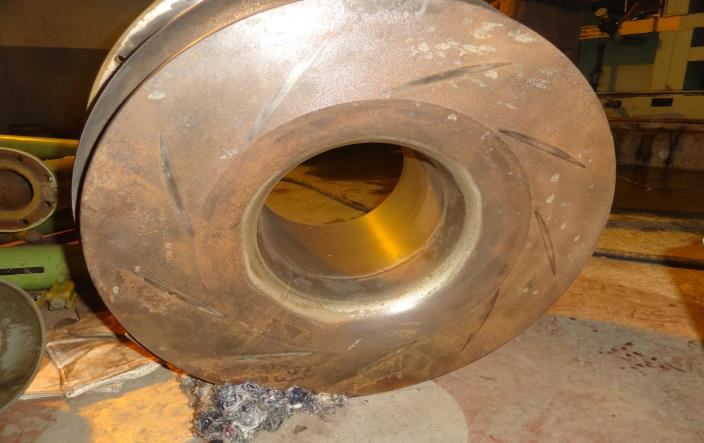

2. 2nd stage scroll — lots of hard dust deposits


3. 3rd stage scroll — cleaning & re-coating


4. 1st stage scroll house — cleaning & re-coating


5. 2nd stage scroll house — cleaning & re-coating


6. 3rd stage scroll house — cleaning & re-coating


7. 1st stage impeller — cleaned, PT check: no defects


8. 2nd stage impeller — cleaned, PT check: no defects


9. 3rd stage impeller — cleaned, PT check: no defects


10. 1st stage cooler — water leakage, cleaned & re-coated


11. 2nd stage cooler — fouled, cleaned & re-coated


Both intercoolers were cleaned and re-coated, and two new air coolers were installed (group 15–16). Cooler aging is the hidden performance killer on 8–10-year-old machines — see our page on intercooler & aftercooler replacement.
12. Bull gear & low-speed gear — tooth flank wear, bull gear replaced with new
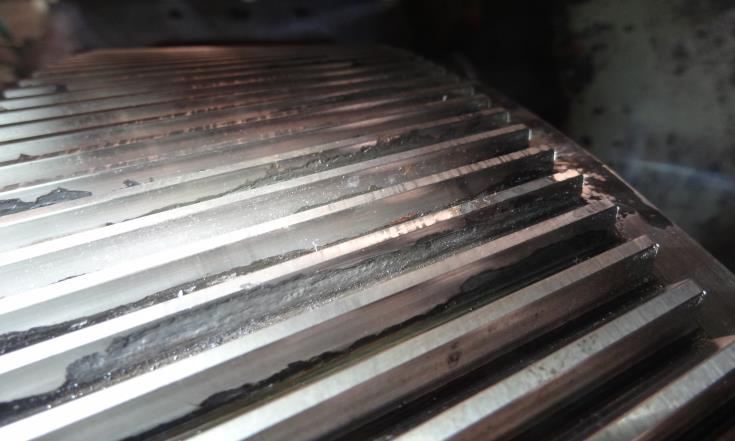

13. Gearbox shafts & tilting pad bearings — cleaned & inspected


14. Shaft bearings & 2nd-stage diffuser — inspected


15. 3rd-stage diffuser & both air coolers — replaced with new


The 3rd-stage diffuser and both air coolers could not be reconditioned — all three were replaced with new units.
16. Air seals & gaskets — replaced; new air cooler ready to install


17. 2nd-stage inlet pipe — cleaning & painting


18. 3rd-stage inlet pipe — cleaning & painting


19. Auxiliaries — link replaced, oil tank cleaned, 2nd-stage inlet cleaned


Measured data — surge test, alignment & probe check
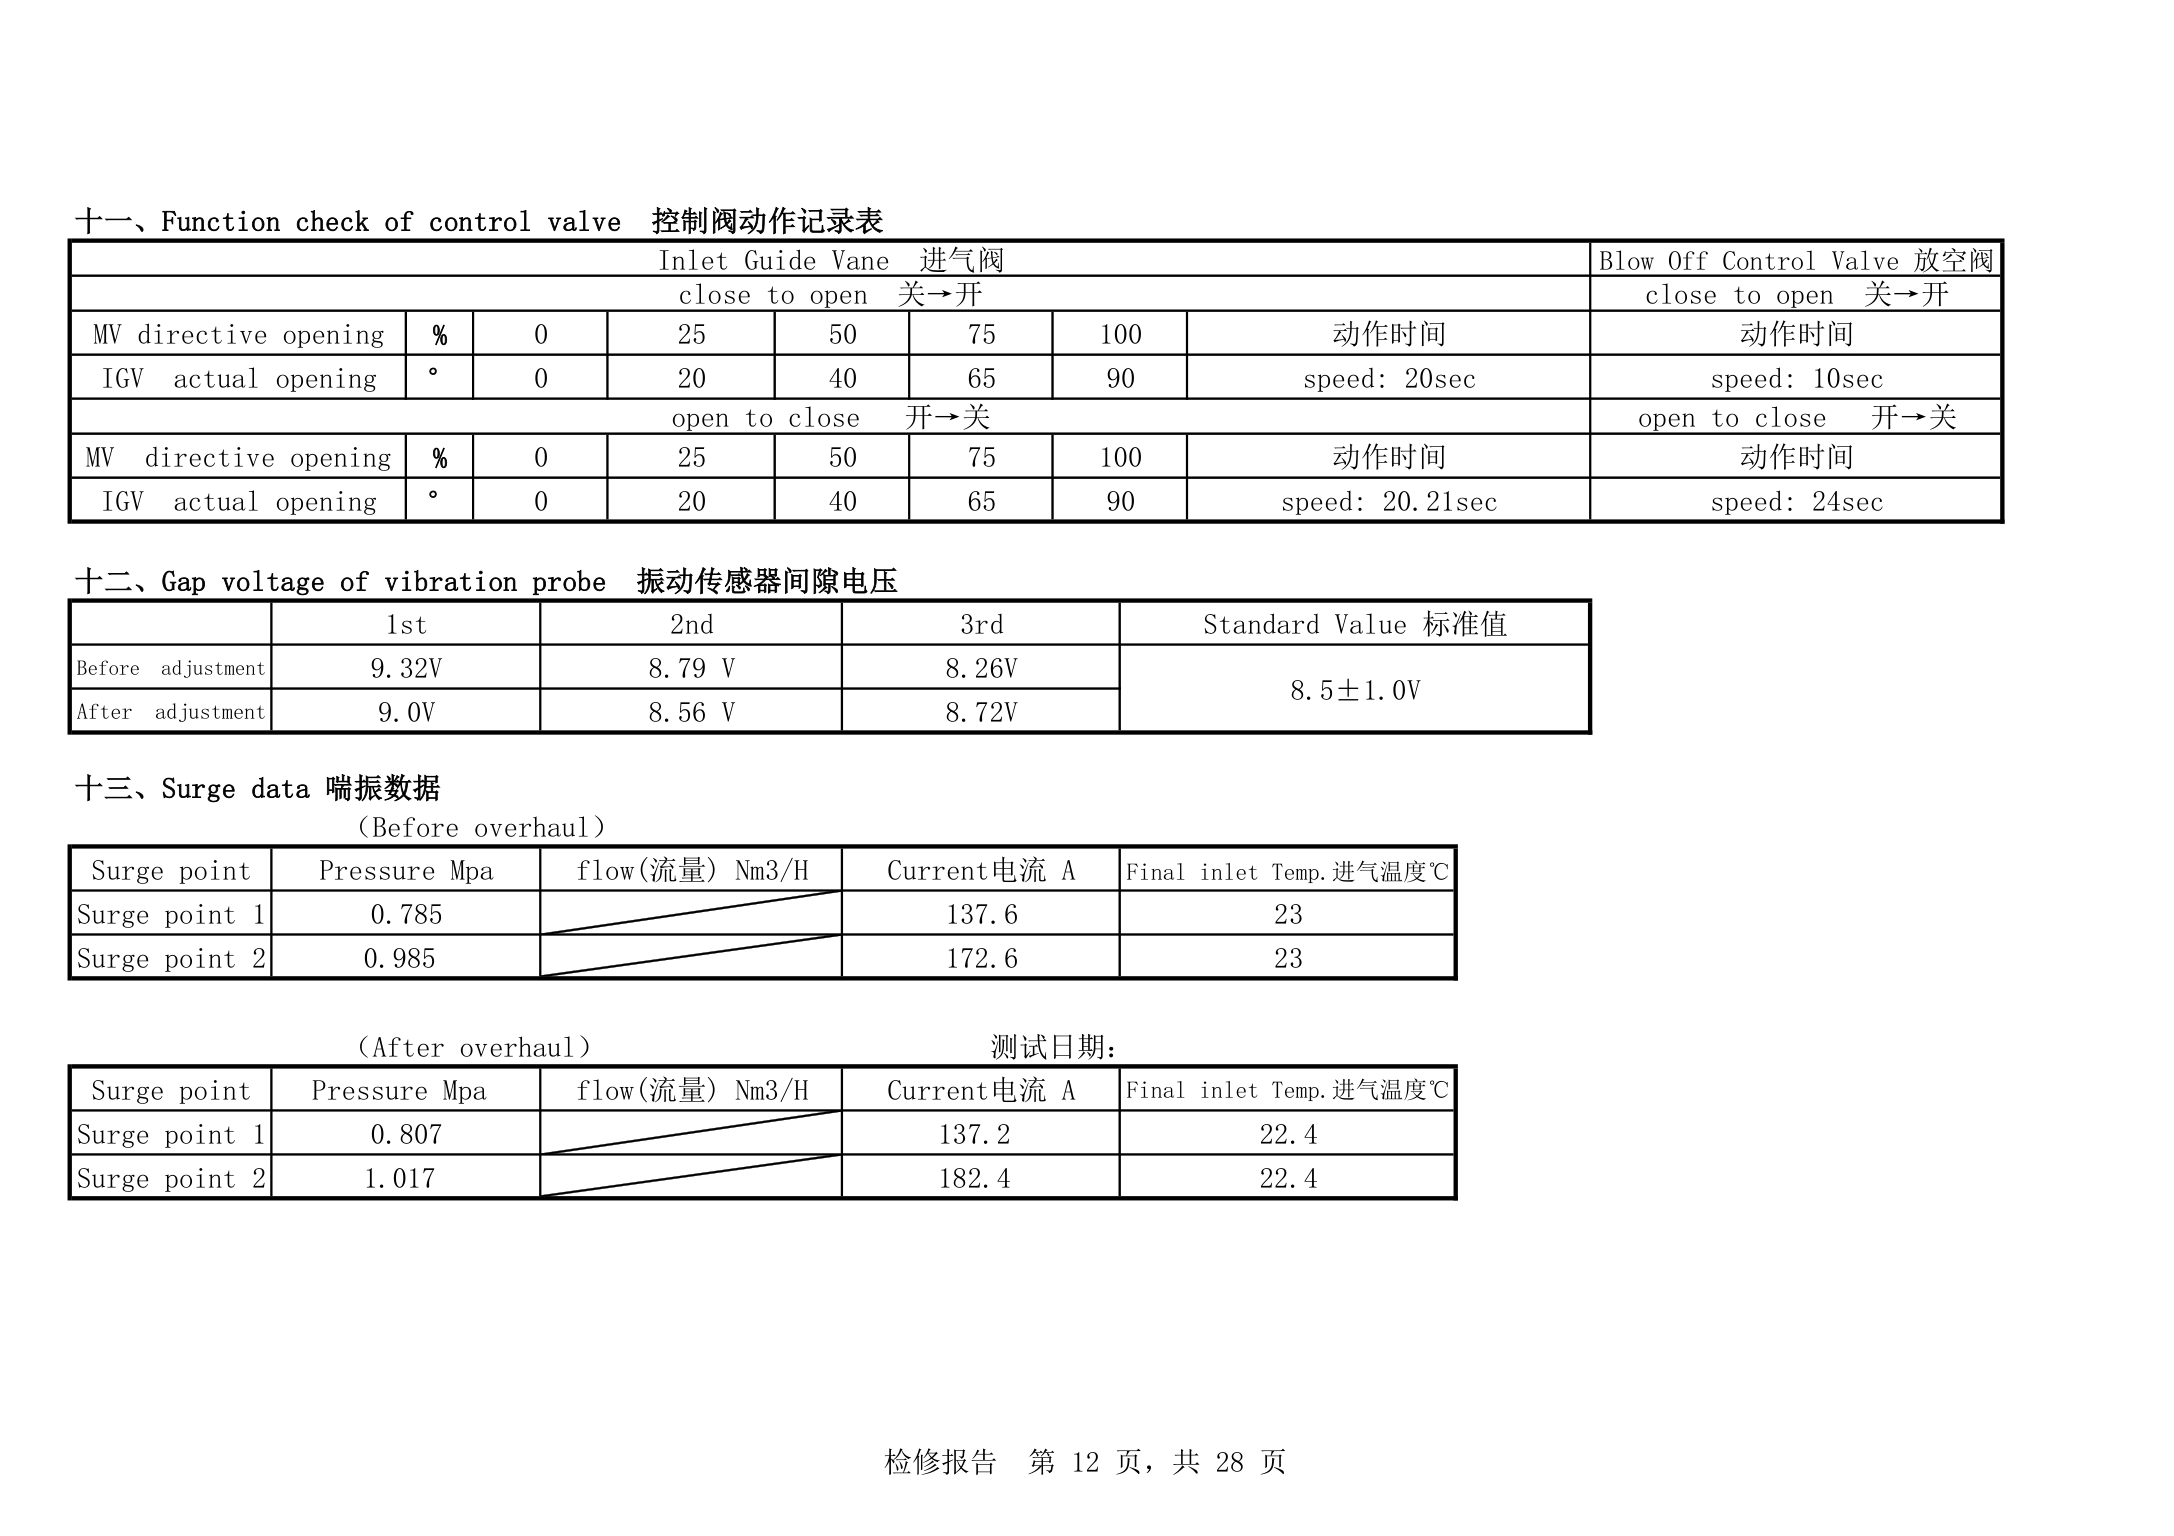
Every overhaul we document with numbers, not only photos. Surge test at the same final inlet temperature, before vs. after overhaul:
Surge test — before vs. after overhaul
| Surge test point | Before overhaul | After overhaul |
| Surge point 1 | 0.785 MPa @ 137.6 A (23 °C inlet) | 0.807 MPa @ 137.2 A (22.4 °C inlet) |
| Surge point 2 | 0.985 MPa @ 172.6 A (23 °C inlet) | 1.017 MPa @ 182.4 A (22.4 °C inlet) |
After the overhaul the machine carries roughly 0.02–0.03 MPa more discharge pressure before reaching surge at the same inlet temperature — the pressure capability lost to fouled impellers, a worn bull gear and a corroded diffuser was restored.
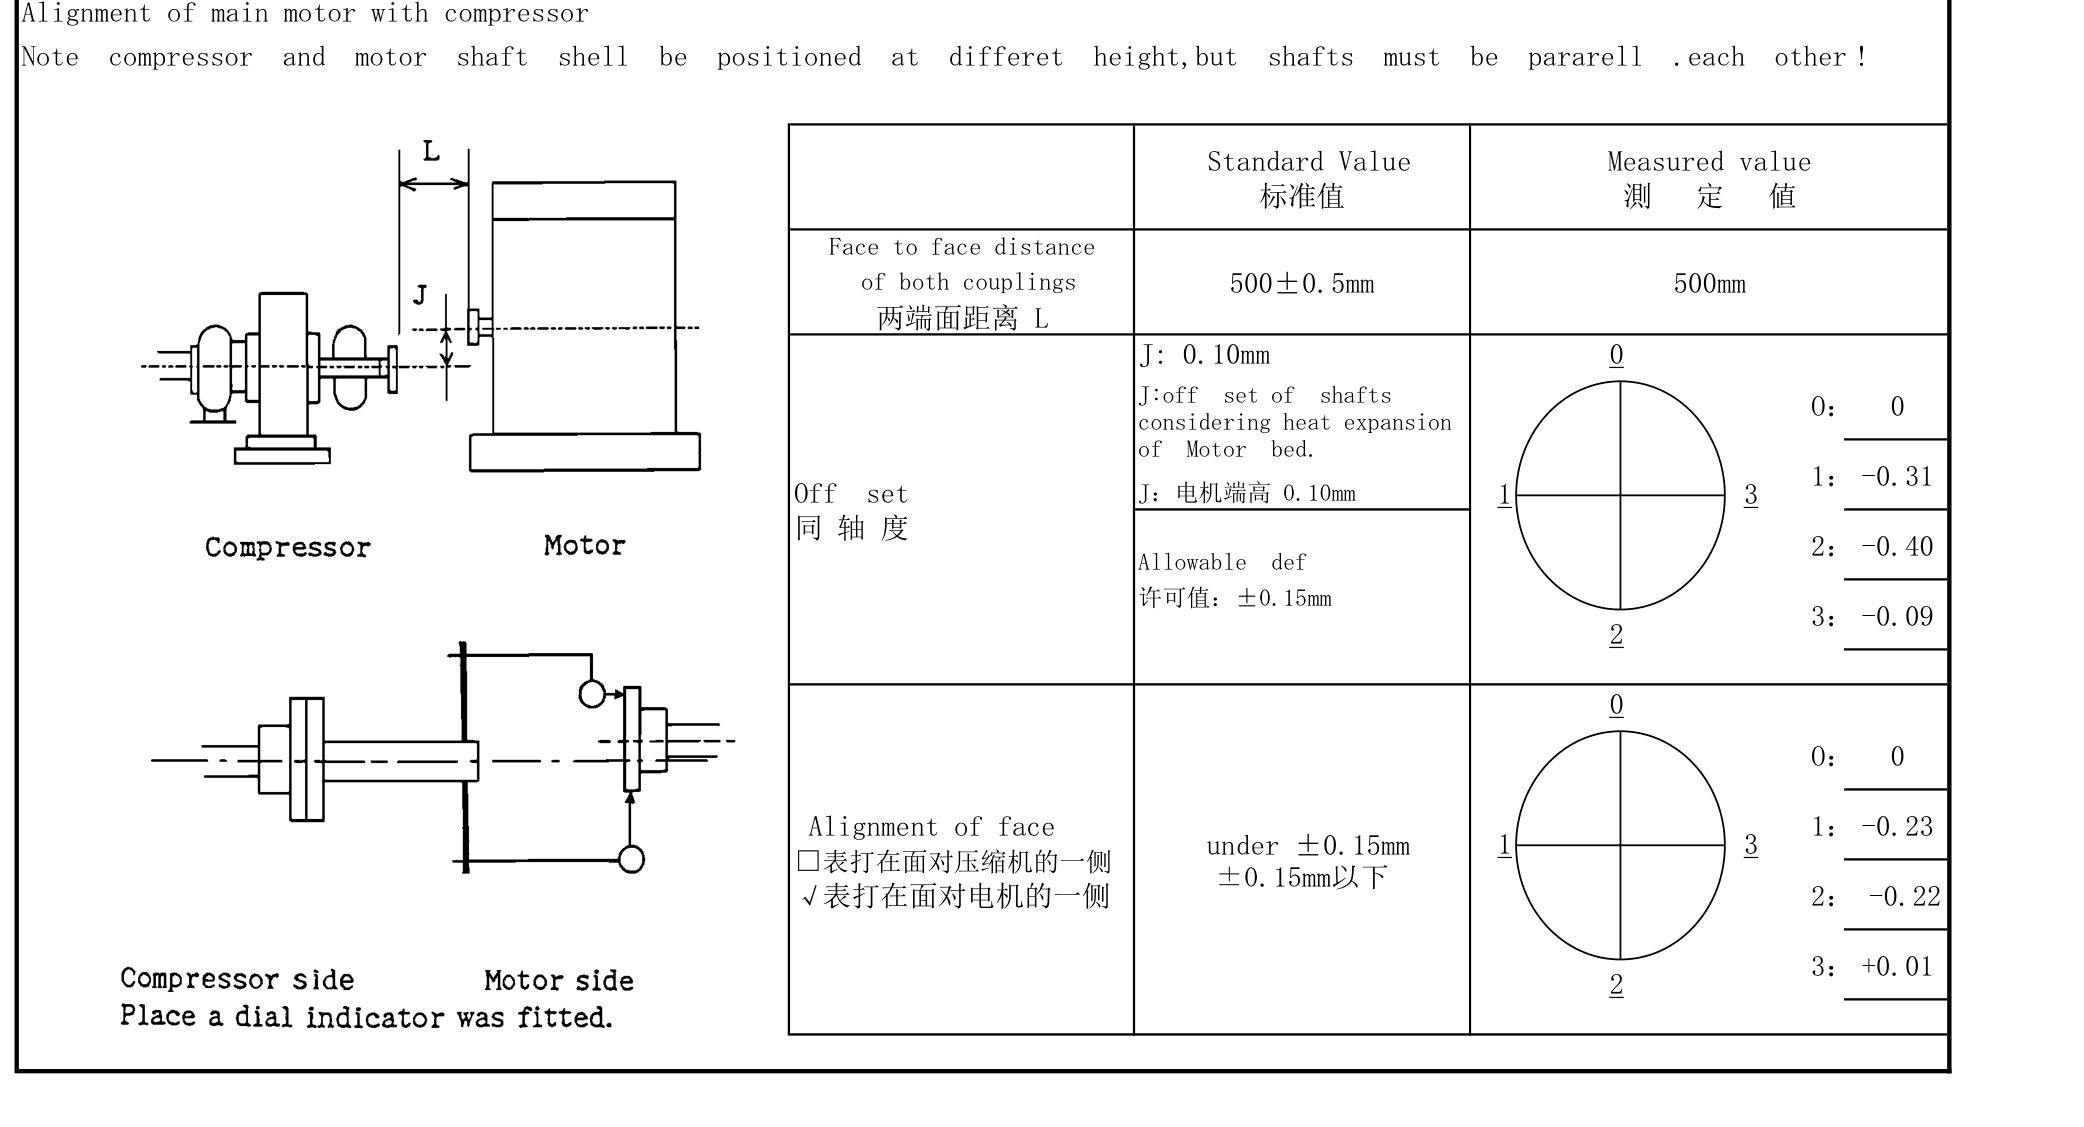
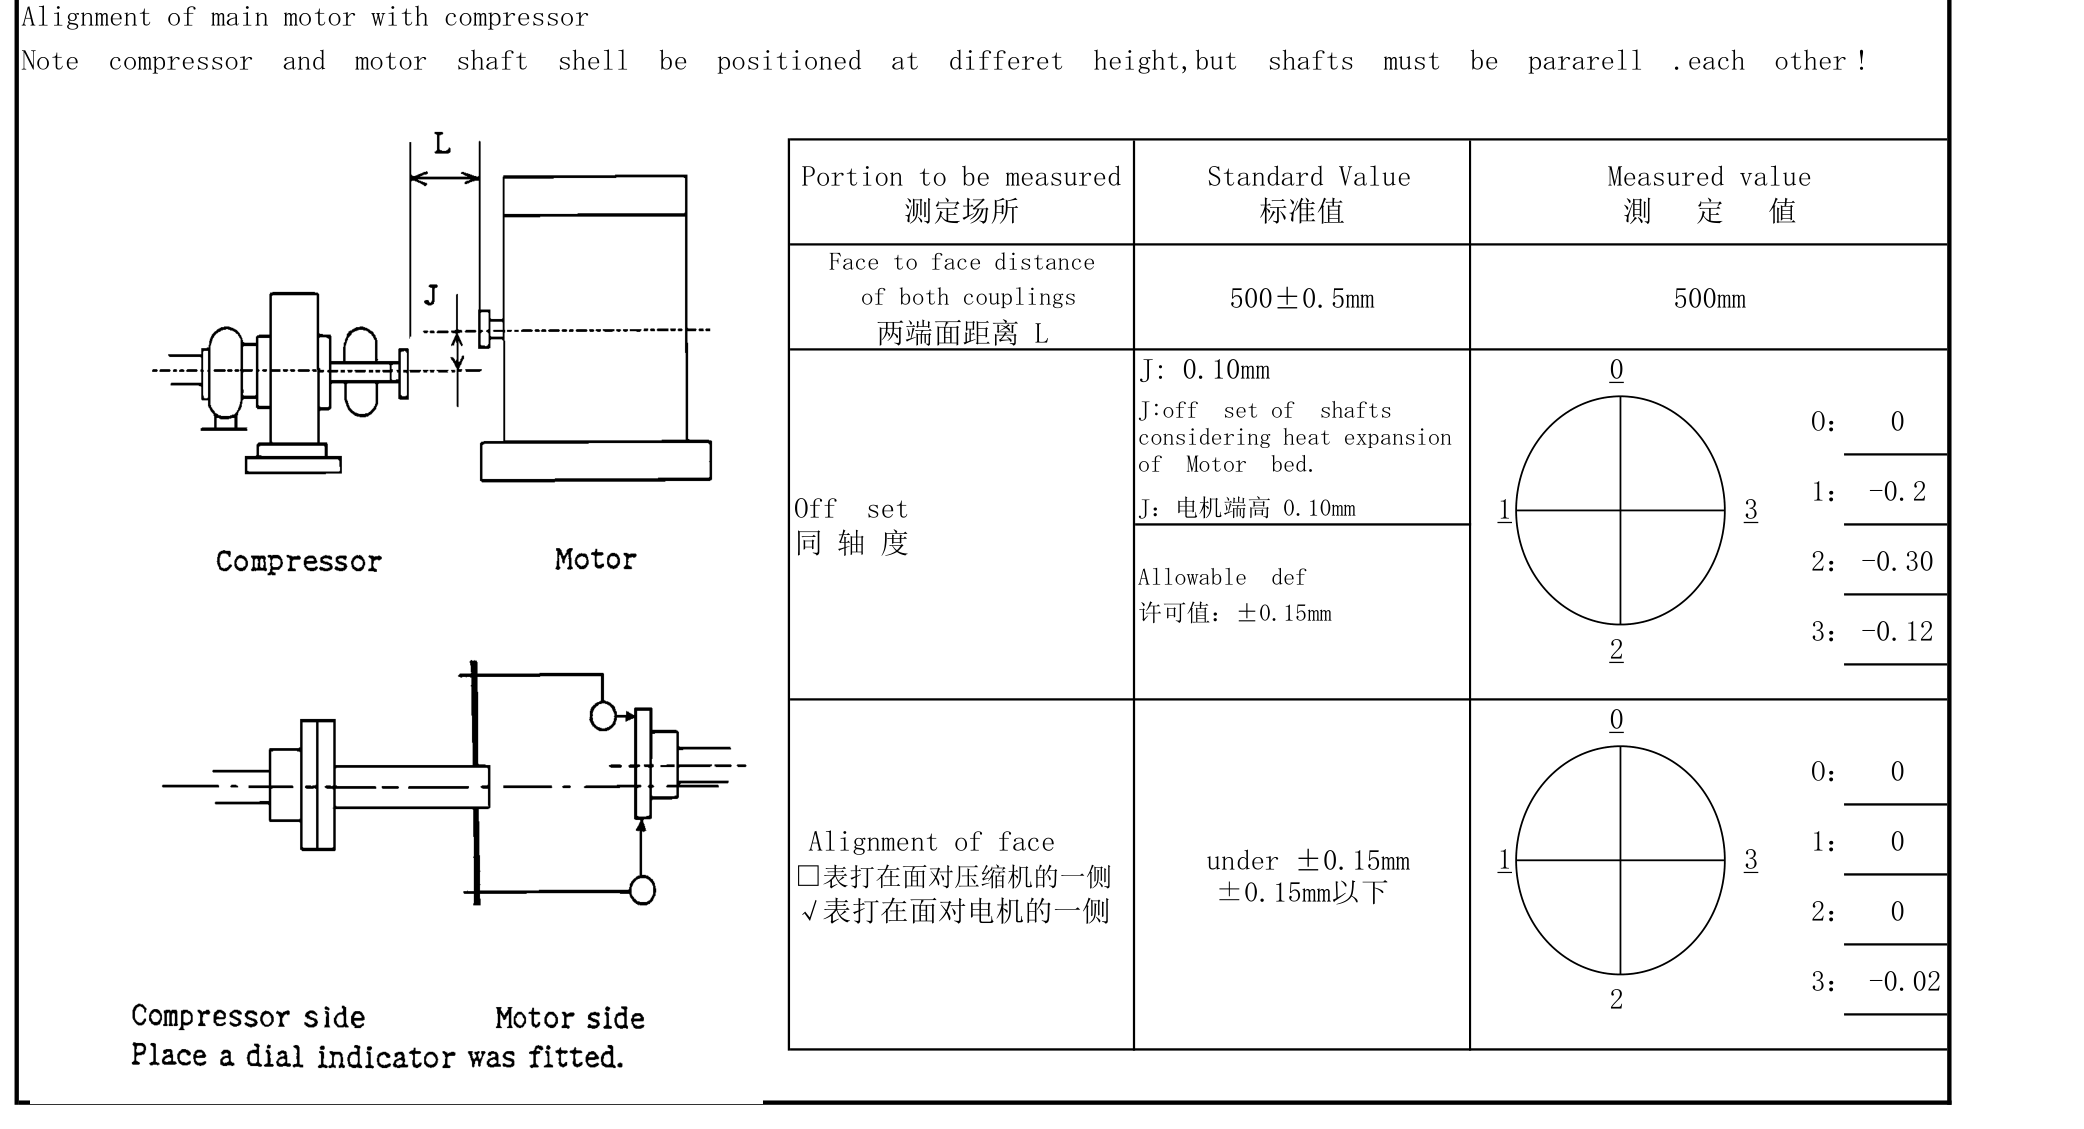
Coupling alignment (motor ↔ compressor, cold)
- Allowable deviation: ±0.15 mm (face & rim); face-to-face distance standard 500 ± 0.5 mm, measured 500 mm
- Face readings improved from −0.23 / −0.22 / +0.01 mm to 0 / 0 / −0.02 mm after alignment
- Motor end kept 0.10 mm high by design, to allow for thermal growth of the motor bed — shafts parallel
- Vibration probe gap voltage: standard 8.5 ± 1.0 V — before adjustment 9.32 / 8.79 / 8.26 V, re-adjusted to 9.0 / 8.56 / 8.72 V, all in range
- IGV travel: open→close 20 s, close→open 20.2 s; blow-off valve function checked
Original alignment record from the overhaul report (cold alignment, before vs. after):
Full inspection record
The overhaul followed the standard IHI inspection checklist. Every item below was opened up and checked — the work actually carried out on each part is listed here.
| Item inspected | Work carried out |
| Air end & gearbox | |
| 1st / 2nd / 3rd stage impellers | Cleaned; PT check — no defects |
| Bull gear & pinion gears | Tooth flank abrasion found; bull gear replaced with new |
| Bull gear shaft bearing | Unusable — replaced |
| High-speed / low-speed pinion bearings | Replaced |
| 1st / 2nd / 3rd stage scrolls & scroll housings | Heavy dust & corrosion — cleaned & re-coated |
| Diffusers | 3rd-stage replaced (heavy gas corrosion); 2nd-stage cavitation — recommended for next overhaul |
| 1st / 2nd / 3rd stage air seals | Replaced with new |
| 1st / 2nd / 3rd stage oil seals | Replaced with new |
| 1st / 2nd / 3rd stage air inlet pipes | Hard dust inside — cleaned & re-coated |
| Coolers | |
| No. 1 intercooler | Fouled; housing leaking — replaced with new |
| No. 2 intercooler | Fouled — replaced with new |
| Oil cooler | Fouled — replaced with new |
| Aftercooler | N/A — not in the machine scope |
| Drain traps & check valve | Inspected |
| Piping & valves | |
| Suction piping | Serious rust — re-coated |
| Discharge & interstage piping | Inspected & cleaned |
| Inlet guide vane / blow-off valve | Function checked, smooth; blow-off spare parts recommended |
| Discharge check valve | Inspected — OK |
| Intake air filter elements | Heavily dust-loaded — replaced |
| Lubrication system | |
| Oil tank | Dirty — cleaned |
| Main / auxiliary oil pumps | Inspected — OK; coupling elements replaced |
| Oil filter | Replaced after oil-line flushing |
| Oil heater & vacuum gauge | Inspected — OK |
| Electrical & controls | |
| Vibration probes | Gap voltage re-adjusted to standard 8.5 ± 1.0 V |
| Protective devices | All simulation function tests OK (see below) |
| Motor terminal screws | Checked & re-tightened |
| Main coupling | Alignment re-done (see data above) |
Alarm & safety function test
| Alarm item | Alarm / trip set point | Result |
| 1st/2nd-stage shaft vibration, upper limit | 40 / 60 μm p-p | OK |
| 3rd-stage shaft vibration, upper limit | 30 / 45 μm p-p | OK |
| Lubrication oil pressure, lower limit | 0.10 / 0.07 MPa | OK |
| Lubrication oil temperature, upper limit | 55 / 60 °C | OK |
| Final-stage intake air temperature, upper limit | 55 / 60 °C | OK |
| Motor bearing temperature, upper limit | 85 / 90 °C | OK |
| Motor stator temperature, upper limit | 120 / 160 °C | OK |
| Motor trouble / auxiliary oil pump trouble signal | — | OK |
Scope of work — parts replaced
- 2 intercooler (air cooler) bundles
- Oil cooler
- 3rd-stage diffuser
- Bull gear
- Bull gear bearing
- High-speed & low-speed pinion bearings
- 1st / 2nd / 3rd stage air seals + O-rings
- 1st / 2nd / 3rd stage oil seals
- Air cooler & oil cooler service kits
- Intake air filter elements
- Oil filter & air breather element
- Oil pump coupling elements
- Temperature & pressure sensors, vibration transducer
- Inlet pipe service kit & gearbox O-rings
In addition: cleaning and protective re-coating of all scrolls, scroll housings and inlet pipes; suction piping re-coated; dye penetrant inspection of all three impellers (no defects); oil-line flushing; coupling alignment within tolerance; vibration probe gap voltage re-adjustment; and a full surge re-test after reassembly.
Post-overhaul operation record
| Item | After overhaul |
| Discharge / system pressure | 0.807–0.809 MPa |
| Motor current | 185 A loaded / 41 A unloaded |
| Oil pressure (before / after filter) | 0.23 / 0.18 MPa |
| Oil temperature | 40 °C |
| No.1 / No.2 intercooler out temperature | 23–24 °C |
| Shaft vibration | 7.6 / 10.1 μm (1st/2nd), 4.6 / 4.7 μm (3rd) |
| Motor bearing / stator temperature | 62–70 °C / 87–89 °C |
The machine was restarted right after the overhaul and all operating parameters were normal — with the new bull gear, coolers and diffuser, the full pressure capability was back.
Root cause & our recommendation
The hard dust came in through the intake filter in the steel-plant environment, and the gas-path corrosion was accelerated by years of condensate. Our recommendations for this machine's next overhaul: replace the 2nd-stage diffuser (early cavitation already visible), keep an air cooler service kit and oil cooler service kit on stock, and watch the pinion bearings. Consumables — air filter elements, oil filter and turbo oil — should be reordered regularly; see our spare parts supplier guide.
Planning an overhaul or need IHI TRX160 spare parts?
Turbomax supplies alternative spare parts and overhaul service kits for the IHI TRX and other IHI centrifugal compressor series — impellers, diffusers, inlet scrolls, bull gears and pinions, air seals, oil seals, journal and thrust bearings, intercoolers & aftercoolers, air filters, oil filters and oil mist separators — and supports overhaul projects worldwide. Our founder has 10 years of IHI-Sullair field service experience. See also our other documented cases: IHI TRE60 major overhaul and IHI TX-A major overhaul.